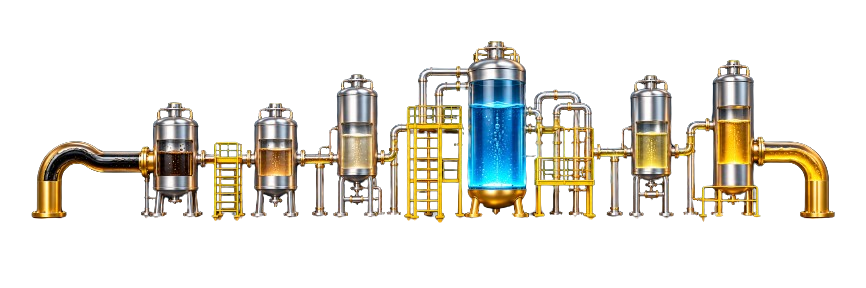
MTF’s patented REEC technology uses water and a proprietary catalyst to transfer hydrogen to complex hydrocarbon feedstocks under atmospheric pressure, converting them into higher-value upgraded hydrocarbon streams.
Atmospheric Pressure
Operates at or near atmospheric pressure for a safer, simpler system.
Moderate Temperature
Effective upgrading at moderate temperatures.
Short Contact Time
Rapid conversion in seconds to minutes.
In-Situ Hydrogen Transfer
Generates and transfers hydrogen from water directly in the reaction.
HOW THE PROCESS WORKS
A Simple, Integrated Process
A continuous catalytic process that upgrades heavy hydrocarbons through a series of integrated steps.
01
Feed Preparation
Condition and prepare heavy feedstock.
02
Water + Catalyst
Introduce water and proprietary catalyst.
03
Catalytic Reactor
Transfer hydrogen to break heavy molecules.
04
Cooling & Separation
Stabilize and separate product streams.
05
Upgraded Products
Higher-value crude, VGO and liquid fuels.
Watch the REEC Technology Film
See how MTF’s catalytic process works — from feed to upgraded products.
✕ Requires separate hydrogen production (e.g., SMR).
✕ Needs specialized high-pressure storage and handling.
✕ Involves complex plant design and integration.
✕ Higher capital, higher operating complexity.
MTF / REEC Catalytic Approach
✓ In-situ hydrogen transfer from water (no separate SMR).
✓ Integrated, simpler process at atmospheric pressure.
✓ Compact and modular system design.
✓ Lower integration complexity and faster deployment.
OUR TECHNOLOGY
PERFORMANCE
THAT CAN BE
MEASURED.
API Gravity (°API)
Before
0
After
0
Viscosity at 50°C (cP)
Before
0
After
0
Sulfur (wt%)
Before
0
After
0
Conradson Carbon (wt%)
Before
0
After
0
Yields
0%
After
0%
CASE EXAMPLE
VTAE CONVERSION AT A U.S. REFINING FACILITY
A practical, scalable approach with real-world operating experience and a track record of safe, reliable performance.
VTAE Processing Using the REEC Technology
Property
VTAE
Product
API Gravity
16.5
42.9
Viscosity @100C
698 cSt
2.0 cSt
Pour point
60 F
-20 F
Conradson carbon
11.0 %wt
0.5 %wt
Ash content
5.3 %wt
<0.01 %wt
Refinery VGO Compatibility (Evaluation Results)
Property
Facility VGO
MTF VGO
Target
Viscosity @40°C (cSt)
21.13
19.15
20–21
Viscosity @100°C (cSt)
4.42
4.17
Report
Viscosity Index
121
122
≥120
CCS @ -25°C (cP)
1,066
867
~1,000
Sulfur (ppm)
247
1,190
—
Silicon (ppm)
14.7
55
—
Chlorine
<200 ppm
<200 ppm
<200
Case Highlights
✓ Converts low-value VTAE into hydrotreater-feed specs.
✓ MTF VGO blend meets hydrotreater feed specs.
✓ Supports increased Group III base oil production.
✓ Demonstrates compelling economics for VTAE conversion.
THE CHALLENGE
Key Constraints
for Heavy Crude.
1.57M gal/yr
VTAE volume
708,651 gal/yr
VGO production
(-45% yield)
673,218 gal/yr
Group III base oil output
(-95% of VGO)
~20%
IRR (modeled)
(-$10.42M project cost)
Annual VTAE revenue (current)
$0K
Annual modeled revenue
$0M
Annual modeled revenue increase
~$0M
A DIFFERENT APPROACH
From Challenging Streams to Higher-Value Products
UPSTREAM: HEAVY & EXTRA-HEAVY CRUDE
Improve crude quality and transportability, with potential to reduce diluent use and expand refinery options.
DOWNSTREAM: VTAE & REFINERY RESIDUALS
Convert lower-value refinery residuals such as VTAE into in to a base oil per-cursor VGO.
VTAE
(Refinery Byproduct)
MTF / REEC
Catalytic Processing
VGO
(Vacuum Gas Oil)
Liquid Fuel
(IBP – 400°F)
Group II and III Base Oil precursor
(increasing ~10x value to the VTAE stream)
ENGINEERED FOR THE FIELD
Proven, Modular and Deployable.
Backed by decades of development and real-world operating experience.
1994
REEC Founded
15+
Patents Registered Worldwide
2012
Commercial Operation
Modular Deployment: From Factory to Field
Fabricate
Test & Validate
Ship (Global Logistics)
Integrate (On-Site)
LET’S EVALUATE YOUR FEEDSTOCK.
Discuss the technical requirements, desired product properties, and integration opportunities with our team.